


A PLC control panel wiring harness is a pre-built, tested set of wires that connects the PLC, I/O modules, terminal blocks, relays and power components inside an enclosure. In a build-to-print order, you supply the design and the manufacturer builds exactly to your documents.
The quality of your RFQ package largely decides three things: how accurate the quote is, how smoothly sampling goes, and how consistent production stays. This guide covers what to send, which specifications matter most for PLC panels, how to write test and acceptance clauses, what drives price, and where projects usually stall.
Harness vs. Machine Cable Assembly: Where the Line Falls
A harness replaces point-to-point hand wiring inside the enclosure. Wires are cut, stripped, crimped, labelled and bundled into branches that follow the panel layout, then tested before they reach the assembly floor.
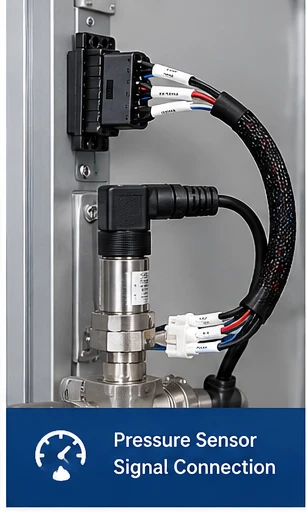
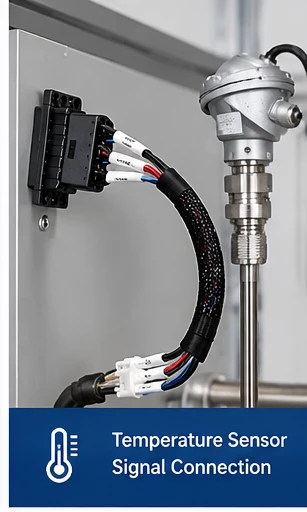
Cables that leave the cabinet are a different product. Motors, sensors and other field devices normally connect through a jacketed, connector-terminated machine cable assembly built for flexing, noise and the shop-floor environment. Many machines need both, and the two are specified differently.

What Build-to-Print Means (and What It Doesn't)
Build-to-print means the customer owns the design. You provide the drawing, bill of materials (BOM), wire list and inspection requirements. The manufacturer builds to them without changing the design, and its job is to confirm the design can be built repeatably, flag risks early and deliver what was agreed.
This differs from build-to-spec, where you define requirements and the supplier proposes the design. It also differs from a supplier-designed product. Build-to-print suits panel builders and machine makers with a proven electrical design who need a repeatable supplier. If your design is unfinished, a manufacturer can help complete the details, but agree in writing who owns the final specification.
What Makes a PLC Panel Harness Different
Most of a PLC panel harness looks like any other low-voltage harness, but a few features of PLC panels should be reflected in your RFQ:
Mixed circuit types in one enclosure. AC power, 24 VDC control, digital I/O and analog signals often share the same panel. Say which wires belong to which group, because separation and routing depend on it.
Wire color by function. IEC 60204-1 is the usual reference for machinery, with common practice being black for power circuits, red for AC control and blue for DC control, plus green/yellow for protective earth. Your local standard or customer specification may differ, so state the scheme you want rather than leaving it to the supplier.
Analog and encoder signals. Low-level signals near drives or contactors are prone to noise. Specify shielded or twisted-pair wire, where the shield terminates, and whether it is grounded at one end or both.
Dense terminal and I/O connections. Many PLC panels use ferrules on stranded wire at spring-clamp or screw terminals, and pre-wired connectors or ribbon-style interfaces on I/O modules. State the ferrule type and length, and the exact terminal or connector model each wire goes to.
Wire identification. Panel technicians troubleshoot from wire numbers. The number on the label must match your schematic and wire list exactly.
RFQ Checklist: What to Send
If some items are not ready, send what you have and flag the gaps. The table separates what is needed to quote accurately from what improves the outcome.
|
Category |
Must have |
Recommended |
Optional / if applicable |
|
Design documents |
Harness drawing or wiring diagram with branch layout; wire list (from, to, wire ID); BOM with manufacturer part numbers |
Panel layout or 3D model showing routing; revision number on every document |
Previous revision history |
|
Wire and components |
Wire gauge, insulation type, voltage/temperature rating, color; terminal, ferrule and connector part numbers |
Approved alternates for each part |
Preferred brands by function |
|
Construction |
Branch lengths and tolerances; labelling method and text format |
Heat-shrink, sleeving, clip and tie positions; wire group separation |
Shielding termination details |
|
Testing and acceptance |
Required electrical tests (see below); workmanship standard |
Sampling plan for crimp pull tests |
Environmental tests for any outside-panel connectors |
|
Compliance |
Target market |
Required declarations (RoHS/REACH, material declarations) |
Customer-specific quality clauses |
|
Commercial |
Annual and per-order quantity |
Packaging and labelling of finished harnesses; delivery terms |
Forecast for next 12 months |
Practical notes on the "must have" items:
BOM and alternates. Manufacturer part numbers, not generic descriptions. Listing pre-approved alternates prevents a stock shortage from stopping the project.
Wire size and rating. Control-circuit wire is often in the range of roughly 0.5–1.5 mm² (about 20–16 AWG), but the right size depends on current, voltage drop, temperature and the standard you follow. State it explicitly for each wire group rather than relying on the supplier's default. Also specify a recognized wire type, for example UL 1007 / UL 1015 style hook-up wire, or the equivalent your market requires.
Tolerances. Give a length tolerance per branch. Branches that are tight in the enclosure but loose on the drawing are a common source of inspection disputes.
Writing Test and Acceptance Clauses
Instead of asking a supplier to "test everything," decide what the harness needs and put it in the RFQ.
Workmanship standard. Name it. IPC/WHMA-A-620 is the widely used standard for cable and wire harness assemblies, and it defines Class 1, 2 and 3 acceptance levels. State the class you require, because it changes inspection criteria for crimps, solder joints (if any), routing and labelling.
Electrical testing.
Continuity and miswire test on 100% of circuits. This checks opens, shorts and swapped positions against your wire list. It is the baseline for any PLC panel harness.
Dielectric withstand (Hi-Pot) and insulation resistance. Specify these when the harness carries mains-level voltage or your customer or standard requires them. For a purely low-voltage 24 VDC control harness they are often not needed, so do not pay for them by default.
Mechanical checks.
Crimp quality. Ask for crimp height verification and pull-out force sampling based on the terminal manufacturer's specification, with a stated sampling frequency.
Visual and workmanship checks. Labels legible and correctly placed, ferrules fully seated, heat-shrink recovered, connector locks engaged.
Environmental tests. IP sealing, temperature cycling or UV aging matter only for connectors and cables that live outside the enclosure. If your order includes those, list them separately from the in-panel harness.
Documentation. Decide whether you need test reports per lot, a first-article inspection report or certificates of conformance, and say so in the RFQ. If your panel will be certified as an industrial control panel (for example under UL 508A in North America), tell the supplier early which components and wire types your certification file relies on. That is a requirement on the parts you specify, not a certification the harness itself carries.
Only Have a Sample or a Photo?
You do not need a perfect drawing to begin. A physical sample, a pinout table or a clear description of each connection can be turned into a drawing and BOM by the manufacturer's engineers, but you should treat that output as a draft until you approve it.
Expect a few questions on wire type, terminal models, routing and labelling. Small differences in panel layout, wire length and labelling convention often show up only when a sample is fitted into a real enclosure, so plan for one fit check before you release volume.
What Drives the Price of a PLC Panel Harness
You will get a more accurate quote, and can compare quotes fairly, if you understand what moves the number:
Wire count and complexity
Each wire adds cutting, stripping, termination, labelling and test time. Wire count usually matters more than total length.
Termination types
Ferrules, ring terminals, multi-pin connectors and shielded terminations each carry different material and labor costs.
Labelling
Printed heat-shrink or sleeve labels with unique numbers on every wire cost more than a single label per branch.
Component sourcing
Named brands with long lead times or low availability affect price and delivery. Approved alternates give the supplier room to optimise.
Testing and documentation
Extra electrical tests, first-article reports and per-lot test reports add time.
Quantity and repeat orders
Setup and programming of test fixtures are spread across the order size. Sharing a 12-month forecast helps.
Ask suppliers to quote on the same basis (same BOM, same tests, same packaging), otherwise the price comparison means little.
From Sample to Production: What to Agree in Advance
Submit
Send your RFQ package. Gaps are fine if flagged.
01
Review
The supplier checks connectors, wire specs, routing, shielding and compliance needs, and lists open questions.
02
Sample
A prototype validates the build process and your fit.
03
Approve and lock
Once the sample is approved, freeze the drawing revision, BOM, inspection points, work instructions and first-article plan.
04
The important rule: there should be no "sample standard" and "production standard." The process, tooling and inspection criteria proven on the sample should carry into volume production. Ask the supplier to confirm this in writing, and ask for first-article inspection on the first production lot.
Common Causes of Delays
Most schedule problems come from information gaps, not from manufacturing
Incomplete BOM or no approved alternates
If a specified terminal is out of stock and no alternate is approved, the job waits.
Wire IDs changed after sampling
Renumbering at the production stage causes relabelling and rework.
Compliance requirements raised late
If the panel is destined for the EU, request RoHS/REACH documents at RFQ stage, not before shipment. Do the same for any North American documentation you need.
Cables added late
If field cables are needed with the panel, include them in the same RFQ so connectors and pinouts are reviewed together.
Unconfirmed tolerances
Agree branch length tolerances before sampling.
Drawing revisions not controlled
Make sure the supplier builds from the current revision, and that changes are issued formally.
FAQ
Q: What is the difference between build-to-print and build-to-spec?
A: In build-to-print, you provide a complete design and the manufacturer builds it as drawn. In build-to-spec, you define performance requirements and the manufacturer proposes the design.
Q: Can I get a quote from a photo or a sample?
A: Often yes for a budgetary quote, but the price firms up only after the manufacturer confirms connectors, wire specs and routing. Treat the first quote as an estimate.
Q: What is IPC/WHMA-A-620 and should I reference it?
A: It is a widely used workmanship standard for cable and wire harness assemblies. Referencing it, along with the acceptance class you need, gives you and the supplier a shared inspection basis.
Q: Do I need Hi-Pot testing on a PLC panel harness?
A: It depends on the voltage and on your customer or standard. Low-voltage control wiring often relies on 100% continuity testing, while harnesses carrying mains voltage commonly add dielectric withstand testing. State it in the RFQ.
Q: What determines the price of a custom harness?
A: Mainly wire count, termination types, labelling, component availability, test scope and order quantity. See the cost section above.